Heavy Duty Super Water Resistant Laminate Flooring Suppliers
Floors in commercial high-traffic areas face a relentless daily routine: thousands of foot passes, ...
Read More


information to be updated
Super water-resistant laminate flooring is a premium product based on water-resistant laminate flooring. With this technology, laminate flooring can be dipped into water for 72 hours, and the swelling rate will be controlled within 5%. Now, this product can be installed in most of the places, even public areas such as coffee shops and restaurants.

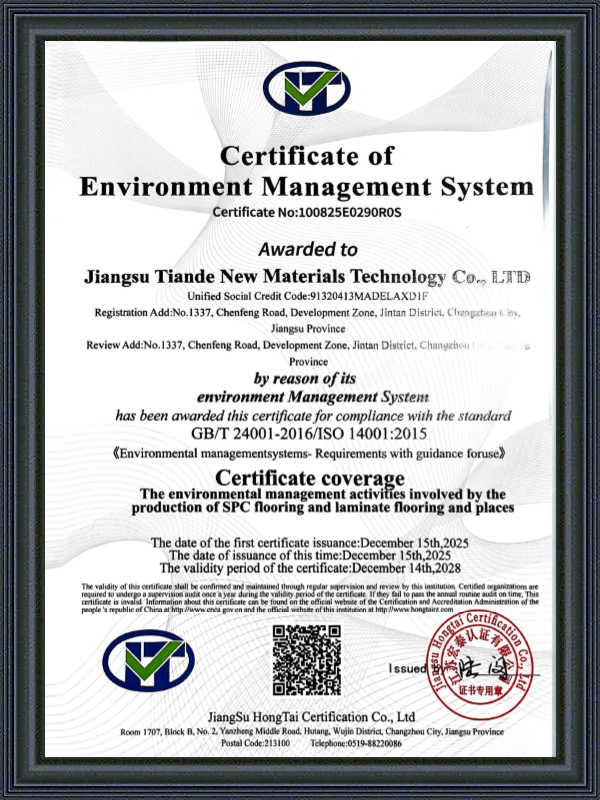
Committed to green and sustainable development, we use high-tech eco-friendly materials to replace natural wood and actively contribute to protecting forest resources and creating a healthier living environment.
Floors in commercial high-traffic areas face a relentless daily routine: thousands of foot passes, ...
Read MoreWalk into any flooring showroom and you will hear "PVC," "vinyl," and "SPC" used almost interchang...
Read MoreWhy Kitchens Demand a Different Approach to Flooring A kitchen floor works harder than almost any o...
Read MoreTraditional laminate flooring has long been appreciated for its realistic aesthetics, durability, and cost-effectiveness. However, its primary vulnerability has historically been moisture exposure. When exposed to liquid spills, humidity, or standing water, standard core boards tend to absorb moisture, leading to edge swelling, surface buckling, and irreversible structural degradation. Recent engineering breakthroughs have fundamentally transformed this material category, giving rise to super water resistant laminate flooring. This advanced surfacing solution bridges the gap between natural wood aesthetics and robust liquid protection.
Super water-resistant laminate flooring is a premium product based on water-resistant laminate flooring. The core technological breakthrough lies in its core composition, surface treatment, and precision edge sealing. With this technology, laminate flooring can be dipped into water for 72 hours, and the swelling rate will be controlled within 5%. This extreme dimensional stability ensures that the planks maintain their structural integrity even during prolonged contact with liquids. Consequently, this product can now be installed in most places, including demanding residential zones and high-traffic public areas such as coffee shops and restaurants.
Residential super water resistant laminate flooring is engineered specifically for modern domestic environments where daily spills, pet accidents, and moisture fluctuations are common. Positioned as a high-performance alternative to traditional hardwood and basic laminate, this category brings peace of mind to homeowners seeking timber visuals without the associated maintenance concerns in kitchens, bathrooms, foyers, and basements.
The core technology of residential-grade planks relies on high-density fiberboard (HDF) with reduced porosity and hydrophobic resin binding agents. Coupled with tight-locking joint profiles and paraffin wax edge coatings, water is prevented from seeping into the core seams. Under standardized testing, planks submerged for 72 hours exhibit a thickness swelling rate well below 5%, ensuring that domestic spills do not cause permanent edge peaking or board warping.
Typical application scenarios include open-plan kitchens, main bathrooms, laundry rooms, and entrance hallways. Unlike standard laminate which requires immediate liquid cleanup, this material tolerates standing moisture for extended periods. Compared to luxury vinyl tile, it offers superior scratch resistance and a firmer, more authentic underfoot feeling that mimics real solid wood.
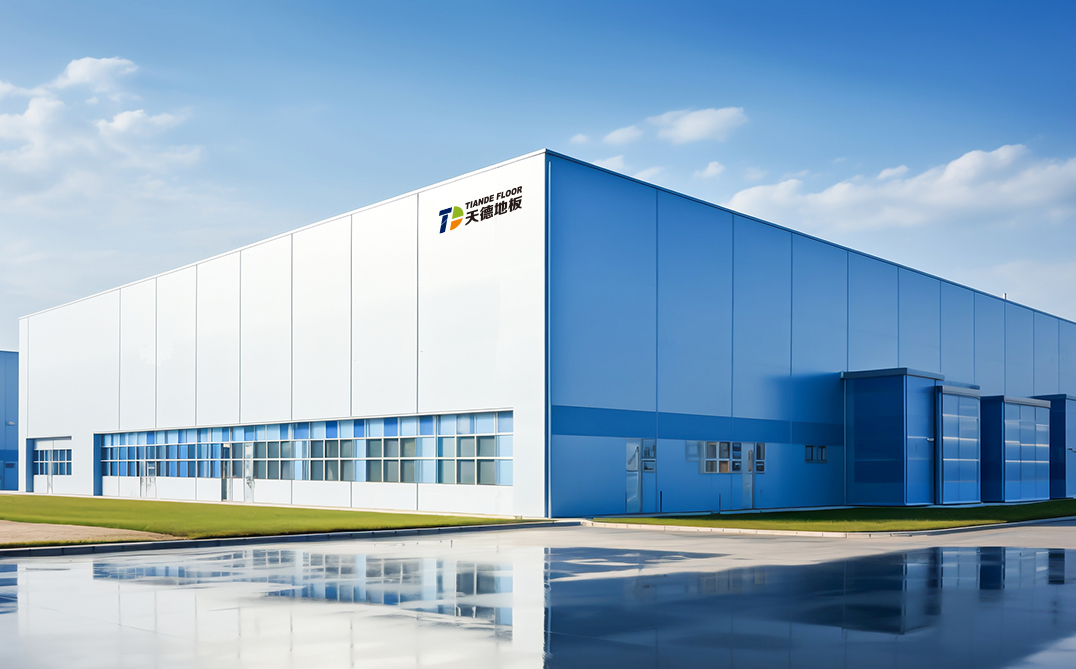
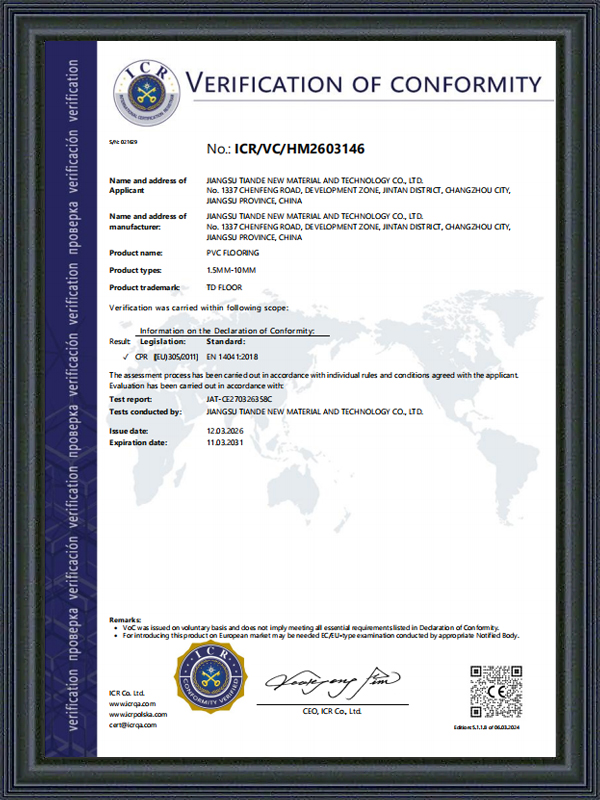
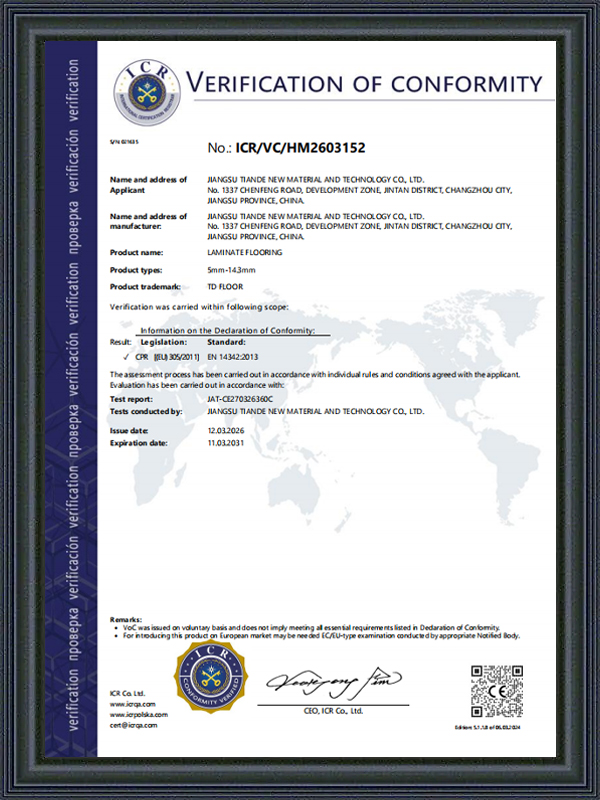
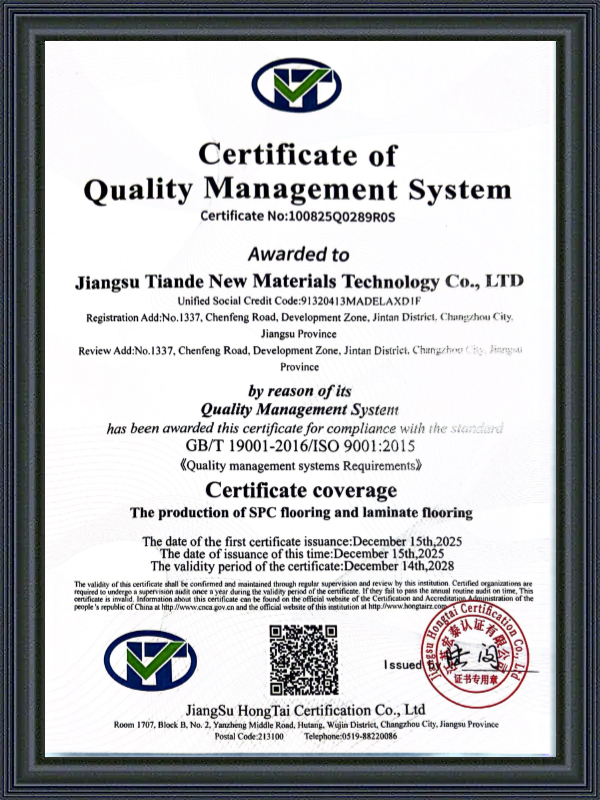
Supporting global residential demand, Jiangsu Tiande New Material and Technology Co., Ltd. specializes in the manufacturing of SPC flooring and laminate flooring for global markets. The company operates a modern manufacturing facility covering 46,000 square meters, supported by automated production equipment and an experienced professional team, ensuring that every residential plank meets stringent international quality standards.
Commercial commercial super water resistant laminate flooring is designed for medium-to-heavy commercial venues that require exceptional wear resistance alongside complete moisture protection. Positioned at the intersection of heavy-duty performance and refined design, this category caters to interior designers, architects, and commercial property owners who demand longevity and minimal maintenance.
Technical features include an elevated AC4 or AC5 wear layer rating combined with ultra-high-density HDF cores. The surface aluminum oxide layer guards against heavy foot traffic, micro-scratches, and roller chair abrasion, while the hydrophobic edge treatment seals vulnerable joint connections. This dual-protection architecture ensures the core remains protected against frequent damp mopping and liquid spills.
Typical application environments include coffee shops, boutique stores, dining areas, hotel lobbies, and corporate offices. In settings like cafes and restaurants where food spills, tracked-in rain, and daily wet cleaning occur continuously, traditional wood or standard laminate quickly fails. This specialized product provides the warmth of real wood without sacrificing hygiene or dimensional stability.
Compared to standard commercial floor coverings, commercial super water resistant laminate flooring delivers lower life-cycle costs and faster installation times. Jiangsu Tiande leverages automated production lines to manufacture high-density commercial planks with tight click-locking tolerances, enabling efficient large-scale rollouts for commercial real estate projects.
Heavy duty heavy duty super water resistant laminate flooring represents the top tier of performance within the laminate industry. Engineered for extreme stress environments, this classification addresses areas subject to intense mechanical loading, rolling loads, high humidity, and frequent surface washing.
The core innovation involves modified thermosetting resins combined with extra-thick HDF cores reaching densities exceeding 880 kg per cubic meter. The interlocking joints feature custom hydrophobic bevel protection that locks out moisture even when joints are subjected to static water pressure. The 72-hour water immersion swelling rate is strictly controlled under 5%, preventing structural delamination even during accidental plumbing leaks or intense commercial cleaning cycles.
Primary application spaces include busy public transport hubs, department stores, educational facilities, healthcare corridors, and large-scale restaurant dining halls. The primary advantage over alternative floorings lies in its combination of realistic surface textures, superior impact resistance, and complete water protection.
To support demanding industrial and commercial requirements, our team brings over 20 years of experience in flooring production and international sales, ensuring stable quality, efficient production, and reliable global supply. Tiande is committed to providing high-quality, environmentally responsible flooring products, while helping partners streamline procurement and improve market competitiveness through one-stop flooring solutions.
| Product Category | Core Density (kg/m3) | AC Wear Rating | 72-Hour Swell Rate | Primary Application Scenarios |
| Residential Grade | 800 - 830 | AC3 / AC4 | Less than 5% | Kitchens, Bathrooms, Living Rooms, Basements |
| Commercial Grade | 840 - 870 | AC4 / AC5 | Less than 5% | Coffee Shops, Restaurants, Retail Boutiques, Offices |
| Heavy Duty Grade | 880+ | AC5 / AC6 | Less than 3% to 5% | Public Terminals, Healthcare Corridors, Shopping Malls |
The performance of modern water-resistant laminate relies on several integrated manufacturing technologies. Below are the primary technical highlights that define this product class:
Achieving long-term water resistance requires strict adherence to standardized manufacturing and installation procedures. The following steps outline the quality protocol:
The low swelling rate is achieved through a combination of ultra-high-density core boards, specialized water-repellent resin binders, and deep hydrophobic edge treatments. This multi-layer protection locks out moisture and prevents core fiber expansion even under direct submersion.
Yes. Because the swelling rate is controlled within 5% during 72-hour water testing, commercial super water resistant laminate flooring can handle frequent liquid spills, wet footwear, and routine commercial damp mopping without warping or edge damage.
Heavy duty super water resistant laminate flooring features higher HDF density (880+ kg/m3), enhanced AC5 or AC6 wear layers, and wax-infused click profile joints. Standard laminate typically swells rapidly when exposed to moisture, whereas heavy-duty water-resistant planks remain dimensionally stable.
Jiangsu Tiande operates a modern 46,000 square meter production facility equipped with automated manufacturing lines. Backed by over 20 years of production and international sales experience, the company maintains strict quality control measures to deliver stable, eco-friendly, and reliable flooring solutions worldwide.